Home/Pipe & Pressure
Pipe & Pressure.
Process piping, hydro-tested emergency repairs, and vessel work — TIG roots, qualified procedures, and paperwork that survives an ASME audit.
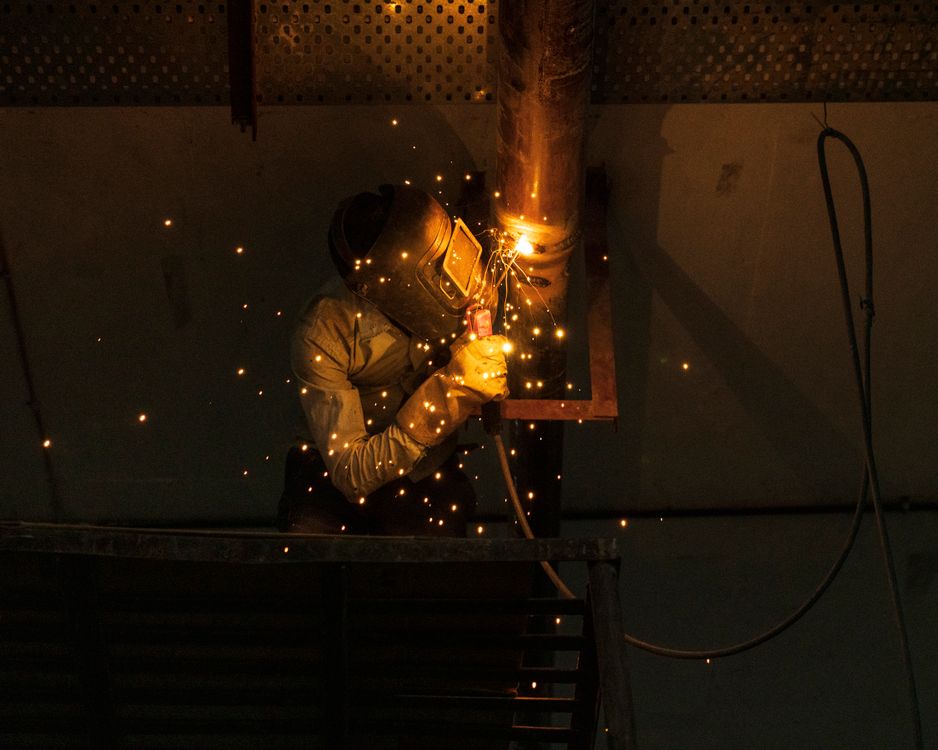 Section IX Qualified Welders
What This Service Covers
Every Joint, Every Time.
Process piping and pressure vessels forgive nothing. Our pipe welders carry current ASME Section IX qualifications across carbon steel, stainless, and chrome-moly — roots laid by TIG for full fusion, fill and cap by MIG or stick to suit position and access.
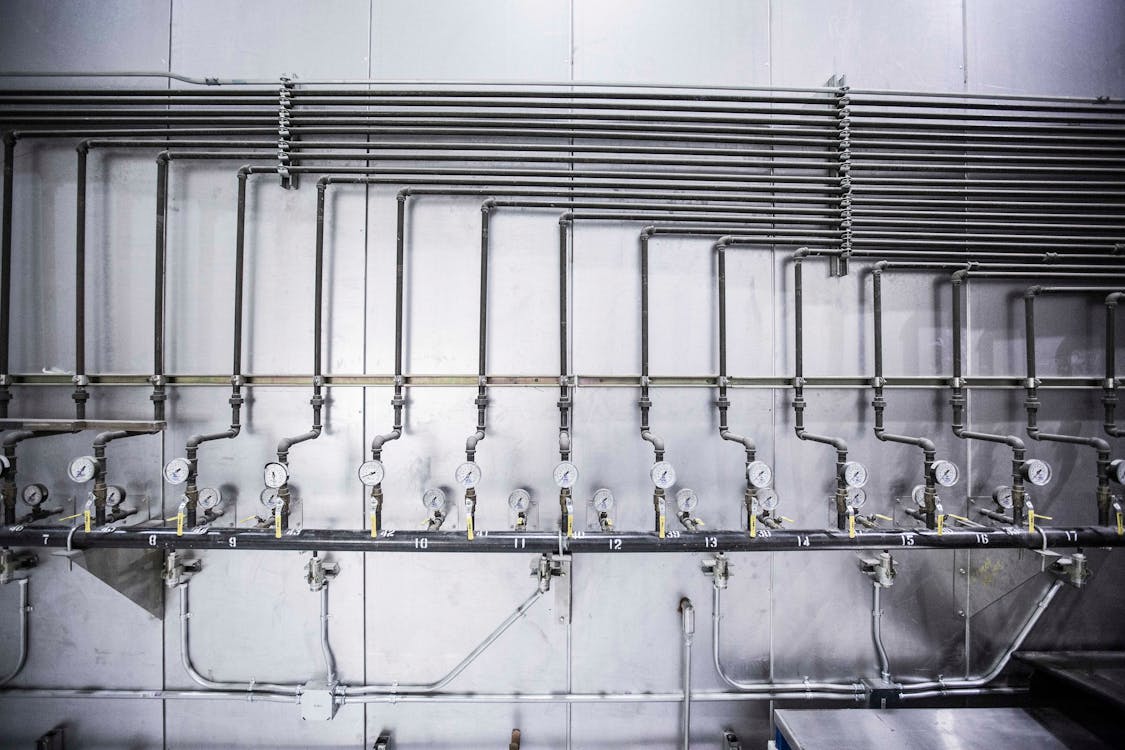
Isolation, purge, preheat, and hydro-test support are part of the job, not extras. You get a line back that holds pressure — with the test charts and weld records to prove it to your insurer and your auditor alike.
What’s Included
Pressure Work, End to End.
Process Piping
Carbon, stainless, and chrome-moly lines from 1/2” instrument tubing to 24” headers.
TIG Roots, X-Ray Quality
Purged stainless roots with full penetration — fit for food-grade, pharma, and high-purity service.
Emergency Line Repair
Leaking spools cut out and replaced root-to-cap, with hydro-test support to get you back online.
Vessel Nozzles & Manways
Nozzle replacement, repads, and manway re-facing per qualified repair procedures.
Purge & Preheat Control
Monitored argon purge and induction preheat with logged temperatures on every critical weld.
Audit-Ready Records
WPS/PQR packages, welder continuity logs, and hydro charts assembled for your QA file.
Process
Isolate. Weld. Prove It.
Isolate & Plan
Lockout scope, line spec, and material confirmed; the qualified procedure is pulled before mobilization.
Prep & Purge
Bevels machined, purge dams set, preheat applied and logged — the weld starts only when conditions are right.
Root to Cap
TIG root with full fusion, hot pass, fill and cap to the WPS — each layer visually accepted.
Test & Document
Hydro or pneumatic test witnessed, charts signed, and the full record package handed over.
Project: Emergency 4” utility loop repair, food plant — hydro passed in 30 hours, zero leaks.
Field Gallery
Recent Pipe Work.

Questions
Pipe & Pressure FAQs.
Which codes and materials do you cover?
ASME Section IX welding for B31.1/B31.3 piping and vessel repair, in carbon steel, stainless (304/316), and chrome-moly. Procedure qualifications are on file and available during vendor approval.
Do you handle hydro testing?
Yes — we support hydro and pneumatic testing up to 1,500 PSI, including gauges, charts, and witnessed holds your QA team can file.
Can you weld shutdown-critical lines on short notice?
Our fastest emergency line repair closed in 36 hours. Call with the line spec and service, and we mobilize with the right procedure already selected.
Do you work in food-grade or sanitary service?
Yes. Purged TIG roots, controlled heat input, and pickle/passivation-ready finishes for sanitary and high-purity lines.
Line down? Talk to us.
Send the line spec, service, and pressure. We’ll confirm the procedure, quote the repair, and schedule the test.